Ultra-High Vacuum Brazing: How Extreme Vacuum Levels Deliver Contamination-Free Joints
23 Sep, 2026
22 Views 0 Like(s)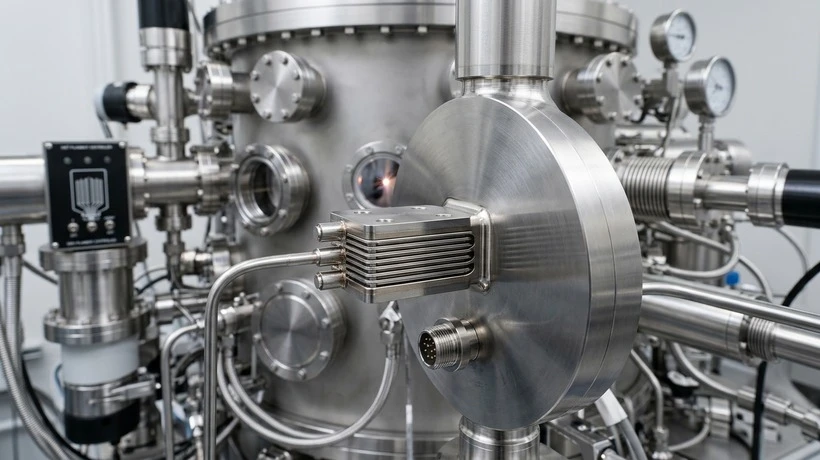
very material inside a UHV furnace becomes a potential outgassing source, so furnace construction, fixturing, and even the filler metal itself have to be selected with vacuum compatibility in mind. Materials with high vapor pressure certain organics, some greases, and even standard-grade stainless steel with retained porosity can outgas enough to prevent the chamber from reaching or holding UHV pressure.
Not every brazing application can tolerate the trace contamination that standard processes leave behind. When a joint is going into a particle accelerator beamline, a semiconductor deposition chamber, or a component made from a reactive metal like titanium or niobium, even the residual gases present in a conventional vacuum furnace can be enough to compromise the result. Ultra-high vacuum brazing exists for exactly this class of problem it pushes vacuum levels far beyond what standard vacuum brazing uses, and that difference in pressure changes what's actually possible in terms of joint cleanliness and metallurgical control.
What Separates Ultra-High Vacuum From Standard Vacuum Brazing
Standard vacuum brazing furnaces typically operate in the range of 10⁻⁴ to 10⁻⁵ torr, which is more than sufficient to remove flux requirements and prevent oxidation for most aluminum, stainless steel, and nickel alloy assemblies. Ultra-high vacuum (UHV) brazing operates several orders of magnitude beyond that, commonly in the 10⁻⁶ to 10⁻⁹ torr range, achieved through turbomolecular or ion pumping systems rather than the mechanical and diffusion pump combinations typical of standard vacuum furnaces.
That gap matters because residual gas molecules oxygen, water vapor, nitrogen, hydrocarbons don't disappear at standard vacuum levels; they're reduced to a level that's acceptable for most engineering applications but still present in measurable quantities. At UHV pressures, the number of gas molecules striking a surface per unit time drops dramatically, which directly affects how quickly a freshly cleaned metal surface can re-contaminate during the heating cycle.
Why Some Applications Require This Level of Vacuum
Reactive and Refractory Metals
Metals like titanium, niobium, tantalum, and molybdenum are highly reactive with oxygen and nitrogen at elevated temperature. Even the residual atmosphere in a standard vacuum furnace can form surface oxide or nitride layers on these metals during the braze cycle, which interferes with filler metal wetting and can embrittle the base material. Ultra-high vacuum brazing reduces this reactive atmosphere enough that these metals can be joined without the surface degradation that would otherwise occur.
Contamination-Sensitive End Uses
Components destined for semiconductor manufacturing equipment, ultra-high vacuum chambers themselves, or scientific instruments often can't tolerate any residual contamination on internal surfaces, since even trace amounts of hydrocarbons or moisture can outgas later and interfere with the sensitive processes those chambers are built to support. A braze joint made under standard vacuum conditions may carry enough surface contamination to become a long-term outgassing source once the component is in service UHV brazing avoids introducing that contamination in the first place.
Hermetic and Long-Service-Life Components
Some hermetic packages certain RF and microwave components, specialized sensor housings, or particle physics instrumentation require an extremely low, stable leak rate over a service life measured in years or decades. Because UHV brazing produces cleaner joint surfaces with fewer trapped contaminants, the resulting bond tends to be more metallurgically consistent, which supports the kind of long-term hermetic stability these applications demand.
Process Considerations Unique to UHV Brazing
Furnace and Fixture Material Selection
Every material inside a UHV furnace becomes a potential outgassing source, so furnace construction, fixturing, and even the filler metal itself have to be selected with vacuum compatibility in mind. Materials with high vapor pressure certain organics, some greases, and even standard-grade stainless steel with retained porosity can outgas enough to prevent the chamber from reaching or holding UHV pressure. Fixtures and hot-zone components are typically built from vacuum-compatible materials such as molybdenum, tantalum, or specially processed stainless steel and graphite.
Bakeout Procedures
Reaching ultra-high vacuum levels generally requires a bakeout step heating the empty or loaded chamber to drive off adsorbed water vapor and other surface contaminants from the chamber walls and fixturing before the braze cycle even begins. Without this step, the chamber can struggle to reach UHV pressure at all, since adsorbed moisture on internal surfaces continues to outgas as pressure drops.
Residual Gas Analysis
Because contamination control is the entire point of the process, many UHV brazing operations incorporate residual gas analysis (RGA) a mass spectrometry technique used to identify exactly which gas species remain in the chamber and at what concentration. This lets operators confirm the chamber has reached the intended vacuum quality and composition before committing a load to the braze cycle, rather than relying on pressure gauge readings alone, which don't distinguish between different gas species.
Filler Metal and Joint Design
Filler metals for UHV brazing are chosen partly for low vapor pressure at braze temperature, since a filler alloy that vaporizes even slightly under vacuum can contaminate both the chamber and the joint itself. Gold-based, palladium-based, and certain nickel or titanium-based filler alloys are common choices depending on the base metals involved and the service temperature the joint will see afterward.
Where Ultra-High Vacuum Brazing Is Used
-
Particle accelerator and beamline components, where internal surfaces must support extremely low pressure over long operating periods
-
Semiconductor processing equipment, including chamber components and internal fixturing exposed to clean processing environments
-
Scientific and research instrumentation, such as mass spectrometers and other vacuum-dependent analytical equipment
-
High-reliability RF and microwave hermetic packages, where long-term leak rate stability is a hard requirement
-
Reactive metal assemblies, including titanium and niobium components used in aerospace, medical, and research applications
Frequently Asked Questions
What vacuum level qualifies as "ultra-high vacuum" in brazing?
Ultra-high vacuum brazing generally operates in the range of 10⁻⁶ to 10⁻⁹ torr, compared to roughly 10⁻⁴ to 10⁻⁵ torr for standard vacuum brazing. The exact threshold varies by industry definition, but the key distinction is the pumping technology required turbomolecular or ion pumps rather than standard diffusion or mechanical pumps.
Why can't standard vacuum brazing be used for titanium or niobium components? Standard vacuum levels still contain enough residual oxygen and nitrogen to form surface oxide or nitride layers on highly reactive metals like titanium and niobium during the heating cycle, which can interfere with filler metal wetting and embrittle the base material. Ultra-high vacuum reduces this reactive atmosphere enough to avoid that degradation.
Does ultra-high vacuum brazing require a bakeout step?
Yes, in most cases. Reaching UHV pressure typically requires baking out the furnace chamber and fixturing beforehand to drive off adsorbed moisture and surface contaminants, since these continue to outgas and prevent the chamber from reaching target vacuum levels otherwise.
What is residual gas analysis used for in UHV brazing?
Residual gas analysis uses mass spectrometry to identify which specific gas species remain in the vacuum chamber and their relative concentrations. It allows operators to verify vacuum quality and composition before running a braze cycle, rather than relying solely on total pressure readings.
How is ultra-high vacuum brazing different from standard vacuum brazing in terms of joint quality?
Because far fewer residual gas molecules are present to re-contaminate a cleaned metal surface during heating, UHV-brazed joints tend to have lower surface contamination and more consistent metallurgical bonding, which supports applications with strict hermeticity, purity, or reactive-metal requirements that standard vacuum brazing isn't suited for.
Comments
Login to Comment